Call us now :+8613306412803
 Send Inquiry

 Send Inquiry
CNC Beam 3D Drilling Machine BT40 Spindles For Steel Structure Application
Price 110000 USD ($)/ Unit
MOQ : 1 Unit
CNC Beam 3D Drilling Machine BT40 Spindles For Steel Structure Application Specification
- Product Type
- CNC Beam 3D Drilling Machine BT40 Spindles For Steel Structure Application
- General Use
- Steel Structure Fabrication
- Material
- Stainless Steel & Cast Iron
- Type
- Drilling Machine
- Capacity
- Max. Drilling Dia 40 mm
- Weight (kg)
- Approx. 11000 kg
- Computerized
- Yes
- Automatic
- Fully Automatic
- PLC Control
- Yes, with Touch Screen Interface
- Bar Feeder
- Automatic Beam Feeding System
- Power Source
- Electric
- Power Consumption
- 25 kW
- Rigidity
- High Rigidity Structure
- Voltage
- 380V / 415V, 50/60Hz, 3 Phase
- Motor
- AC Servo Motor
- Table Size
- Customizable as per beam size
- Spindle Speed
- 50-3000 rpm (Stepless) - BT40 Spindle
- Axial Choice
- 3 Axis (X, Y, Z)
- Dimension (L*W*H)
- 8000 mm x 2600 mm x 2900 mm
- Feature
- Low Energy Consumption, High Speed, High Precision
- Color
- Blue & White
- Warranty
- Yes
- Applicable Profiles
- H-Beam, Channel Steel, Angle Steel
- Clamping Method
- Hydraulic Clamping System
- Safety Features
- Emergency Stop, Interlocking Guard Doors
- Working Environment
- 0-40C; Humidity 80%
- Coolant System
- High Pressure Through-Spindle
- Operator Interface
- Touch Screen 15" HMI
- Network Connection
- Ethernet, USB Support
- Air Supply
- 0.5 - 0.8 MPa
- Control System
- SIEMENS PLC with Remote Monitoring
- Min Beam Size
- H 200 x W 75 mm
- Drilling Accuracy
- 0.1 mm
- Tool Changer
- Automatic, 3x6 Tools per Spindle
- Max Feeding Speed
- 30 m/min
- Spindle Amount
- 3 Spindles (Top, Left, Right)
- Max Beam Size
- H 1500 x W 630 mm
CNC Beam 3D Drilling Machine BT40 Spindles For Steel Structure Application Trade Information
- Minimum Order Quantity
- 1 Unit
- Supply Ability
- 10 Units Per Day
- Delivery Time
- 30 Days
CNC Beam 3D Drilling Machine BT40 Spindles For Steel Structure Application About
Product Features
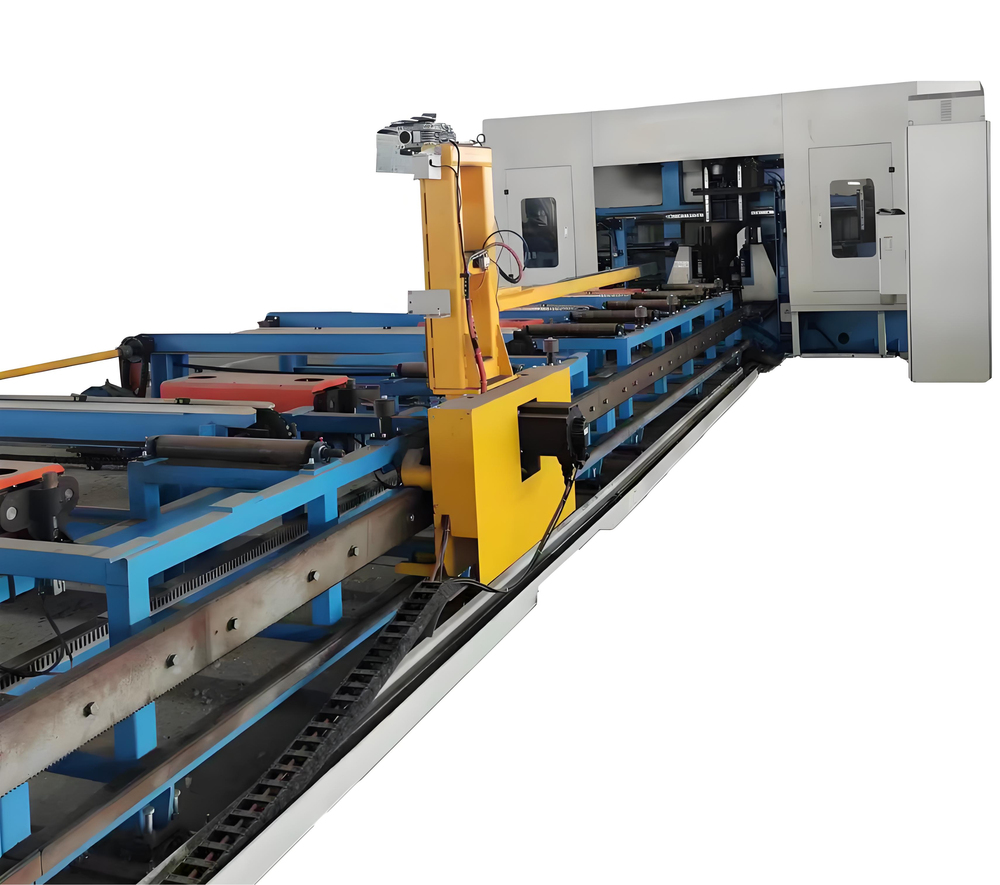
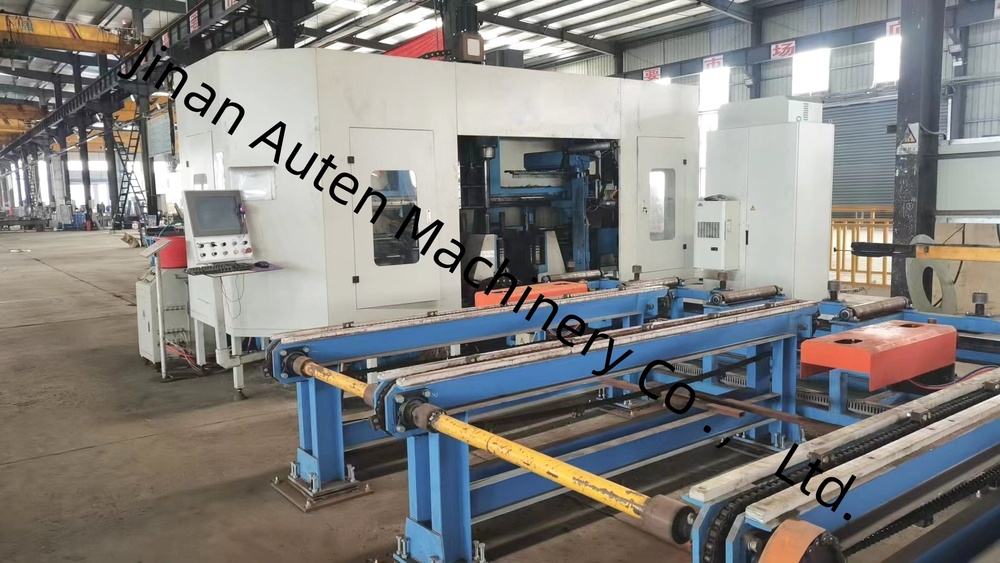
1. This 3D H-beam drilling and cutting machine is primarily composed of the main machine body, CNC feeding system, material conveyor, electrical system, hydraulic system, cooling system, lubrication system, waste bin, and other integral components. Featuring a fixed bed structure with a movable workpiece setup, the machine is ideally suited for processing large H-beams. It supports continuous production and is distinguished by its advanced level of automation.
2. The drilling machine body comprises the bed, CNC sliding table assemblies, support devices, upper and side pressing units, and detection systems. The CNC sliding table components include the fixed side, movable side, and the upper-unit CNC sliding table. Specifically designed for H-beam drilling operations, the sliding table assemblies are made up of a sliding plate, sliding table base, spindle headstock, high-speed mechanical spindle, tool cylinder, variable-frequency motor, servo motor, linear guides, and lead screws.
3. The CNC feeding system consists of brackets, gears, racks, servo motors, reducers, and manipulators. The servo motor drives the manipulator, facilitating the X-direction movement of the H-beam, thus ensuring accurate feeding and precise positioning of the workpiece.
4. The material conveyor is comprised of both an in-feeding conveyor and an out-feeding conveyor. The in-feeding conveyor includes conveyor brackets, support rollers, and side-pushing devices, specifically designed to transport profiled steel blanks, achieve Y-direction positioning of the blanks, and work in conjunction with the CNC feeding system to complete the material feeding process. The out-feeding conveyor, made up of material channel brackets and support rollers, is dedicated to the transportation of finished workpieces.
5. The cooling system utilizes both internal and external cooling methods, employing oil mist to cool the borehole. This approach offers several advantages, including reduced coolant consumption, promoting cost efficiency, environmental sustainability, and minimizing drill bit wear.
6. The hydraulic system is responsible for powering the upper pressing device, side pressing device, tool cylinder, and other associated components.
7. The pneumatic system is designed to supply power to the manipulator, testing cylinder, and other comparable equipment.
8. The lubrication system combines both centralized and manual lubrication methods. Centralized lubrication is primarily used for the timed and precise lubrication of the main linear guides and lead screws.
9. The machine tool's control system consists of a host computer, PLC, and other related components. Programming Method: Processing programs are generated by inputting CAD drawings or processing parameters via a USB interface or keyboard. These programs can be stored, retrieved, displayed, and transmitted at any time based on part numbers. The system not only allows for manual adjustment and control of individual processing parameters but also enables full automation of the entire processing workflow.
Advanced Multi-Spindle Technology
With three powerful BT40 spindles positioned on the top, left, and right, this machine allows efficient and simultaneous drilling of beams and structural profiles. The high rigidity structure ensures both stability and precision during operations, reducing cycle times and improving throughput.
Precision Engineering for Steel Fabrication
Engineered for tight tolerances, the machine achieves drilling accuracy up to 0.1 mm. The automatic hydraulic clamping system and high-pressure through-spindle coolant maintain optimal bite and cooling, resulting in consistent high-quality holes for critical structural applications.
Effortless Automation and User Control
Controlled by SIEMENS PLC, operators enjoy full command via a 15-inch HMI touch screen. The automatic beam feeder, tool changer, and network connectivity (Ethernet/USB) make operation seamless and highly productive. Remote monitoring further enhances oversight and maintenance.
FAQ's of CNC Beam 3D Drilling Machine BT40 Spindles For Steel Structure Application:
Q: How does the CNC Beam 3D Drilling Machine improve steel structure fabrication efficiency?
A: The machine features three BT40 spindles, automatic tool changers, and an automatic beam feeding system. This combination enables simultaneous multi-side drilling, quick tool changes, and rapid material handling, significantly accelerating production while maintaining high precision.Q: What profiles and materials can be processed with this machine?
A: It is engineered for H-beams, channel steel, and angle steel made of stainless steel or cast iron. Its robust hydraulic clamping and high rigidity structure accommodate beams from H 200 x W 75 mm up to H 1500 x W 630 mm.Q: Where can this CNC drilling machine be installed and operated?
A: Ideal for steel fabrication workshops and manufacturing plants, the machine works efficiently in controlled environments with temperatures from 0 to 40C and humidity up to 80%. Its power requirements are 380V/415V, 50/60Hz, 3-phase supply.Q: What is the process for changing tools and maintaining productivity?
A: Each spindle supports automatic tool changing with 3x6 tools available. This setup enables non-stop operation, minimal changeover delays, and consistent drilling by automatically selecting and swapping the necessary tools according to the job program.Q: What safety features are included to protect the operator?
A: Safety is prioritized with emergency stop buttons, interlocking guard doors, and an enclosed design. These prevent accidental contact and ensure the machine halts immediately in case of emergencies, safeguarding personnel and equipment.Q: How does the control system enhance machine operation?
A: The SIEMENS PLC system offers intuitive control via a 15-inch touch HMI. Remote monitoring, Ethernet, and USB connectivity enable seamless integration with company networks, facilitate real-time data access, and allow efficient troubleshooting and remote assistance.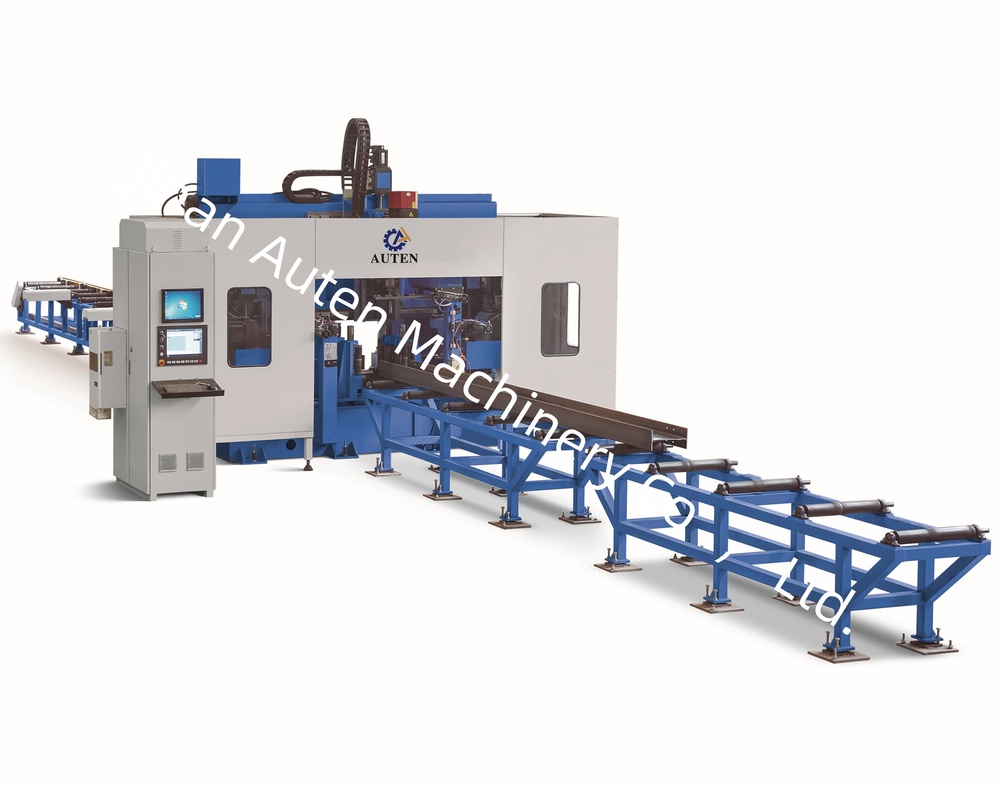
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in CNC H Beam Drilling Sawing Machine Line Category
Space Frame Structure CNC I Beam Drilling Machine Prefabricated Steel Buildings
Price 110000 USD ($) / Unit
Minimum Order Quantity : 1 Unit
Voltage : 380V/415V, 3 Phase
Computerized : Yes
Axial Choice : 3 Axis CNC Control
Capacity : H Beam 150mm1500mm
3-Spindle CNC Vertical H-Beam Drilling Marking and Cutting Machine
Price 115000 USD ($) / Unit
Minimum Order Quantity : 1 Unit
Voltage : 380V/415V, 3 Phase, 50/60Hz
Computerized : Yes
Axial Choice : Three Spindles (X, Y, Z)
Capacity : Web height: 2001500 mm, Flange width: 100800 mm
High Speed CNC Gantry Large Steel Metal Plate H Beam Drilling Machine for Steel Structure
Price 132000 USD ($) / Unit
Minimum Order Quantity : 1 Unit
Voltage : 380V/50Hz 3Phase (Customizable)
Computerized : Yes
Axial Choice : X/Y/Z Axis CNC Control
Capacity : Drilling Plate Thickness up to 100 mm
Cost-Saving H Beam CNC Drilling and Sawing Machine Line
Price 200000 USD ($) / Unit
Minimum Order Quantity : 1 Unit
Voltage : 380V/415V 3Phase
Computerized : Yes
Axial Choice : 3 Axes (X, Y, Z)
Capacity : Supports Beams up to 1500mm Height

 Send Inquiry
Our Products


2301, Building 1, Fortune Plaza, No.2177, Tianchen Road,Jinan - 250000, Shandong, China
 : 8613306412803

Mr Gaven
(Marketing Director )
Mobile :+8613306412803
 Send Inquiry
 Call Me Free

Developed and Managed by Infocom Network Private Limited.
